Case Studies · G
Alumina Industrial Heat-Sink Part
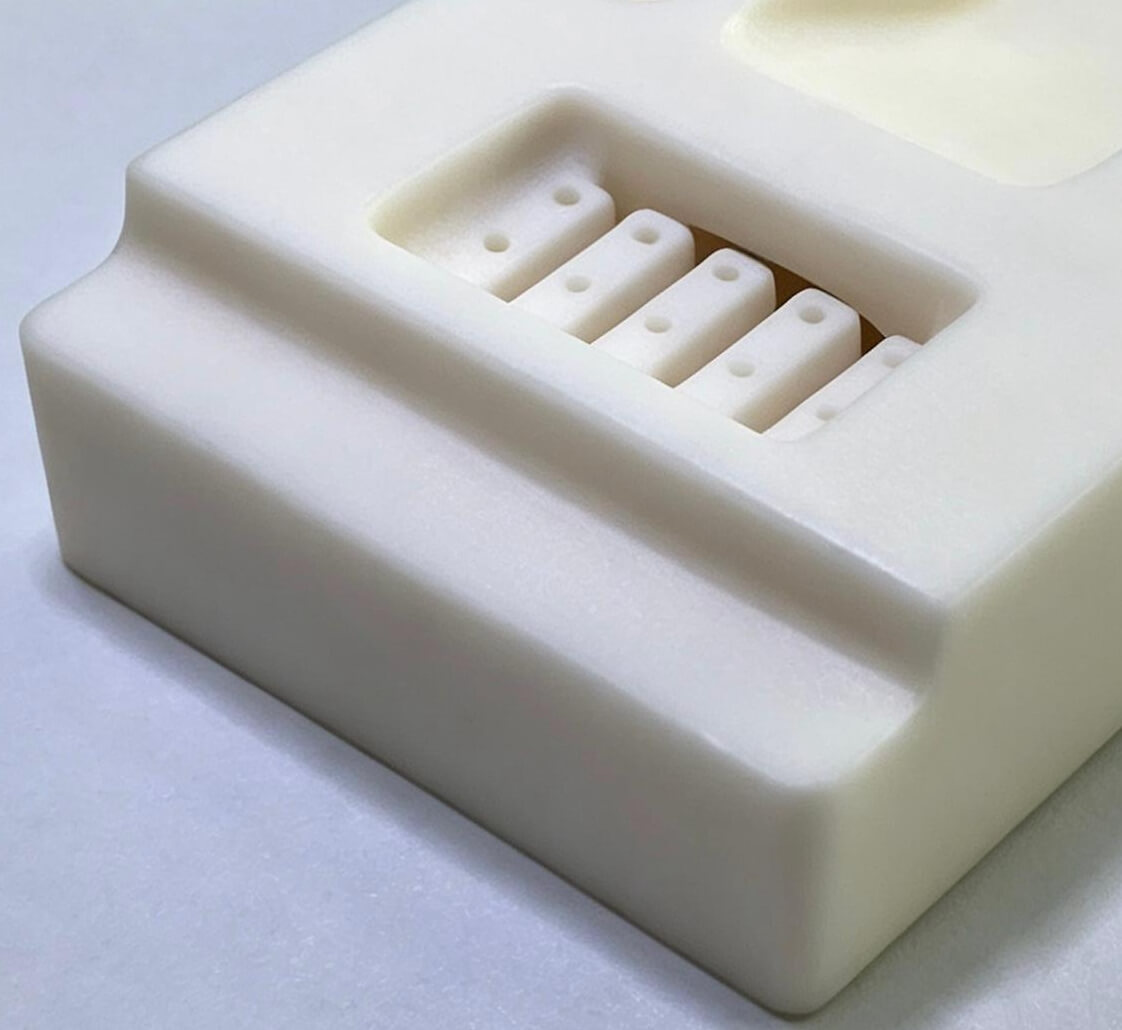
Difficulty: the base mounting wall is 4.8mm thick, far past the typical 0.7-1.5mm sink-safe range, already carrying elevated internal-porosity risk; at a 4.8:1 wall-thickness ratio, the open-frame structure also amplifies distortion risk from green-body density gradients during sintering. Two factors stacked to push warpage risk to an extreme. At a more microscopic material level, alumina's own particle size runs larger than zirconia's and its particle-size distribution is less uniform, which makes sintering shrinkage itself less consistent - a third layer of cause stacked on top of the structural factors. This is the real project documented in WP-05 - three gate-plan iterations, from 0% to 100% yield.
Solution: three rounds of gate-plan iteration converged on a three-face centripetal-flow gate design, proactively relocating the low-density flow zone to a non-functional area. Moldflow + short-shot + OGP + CT four-way verification, 200-piece batch yield 100%, flatness ±0.019mm.