Case Studies · A
Ultra-Thin Wall + A-Grade Gloss, Coexisting
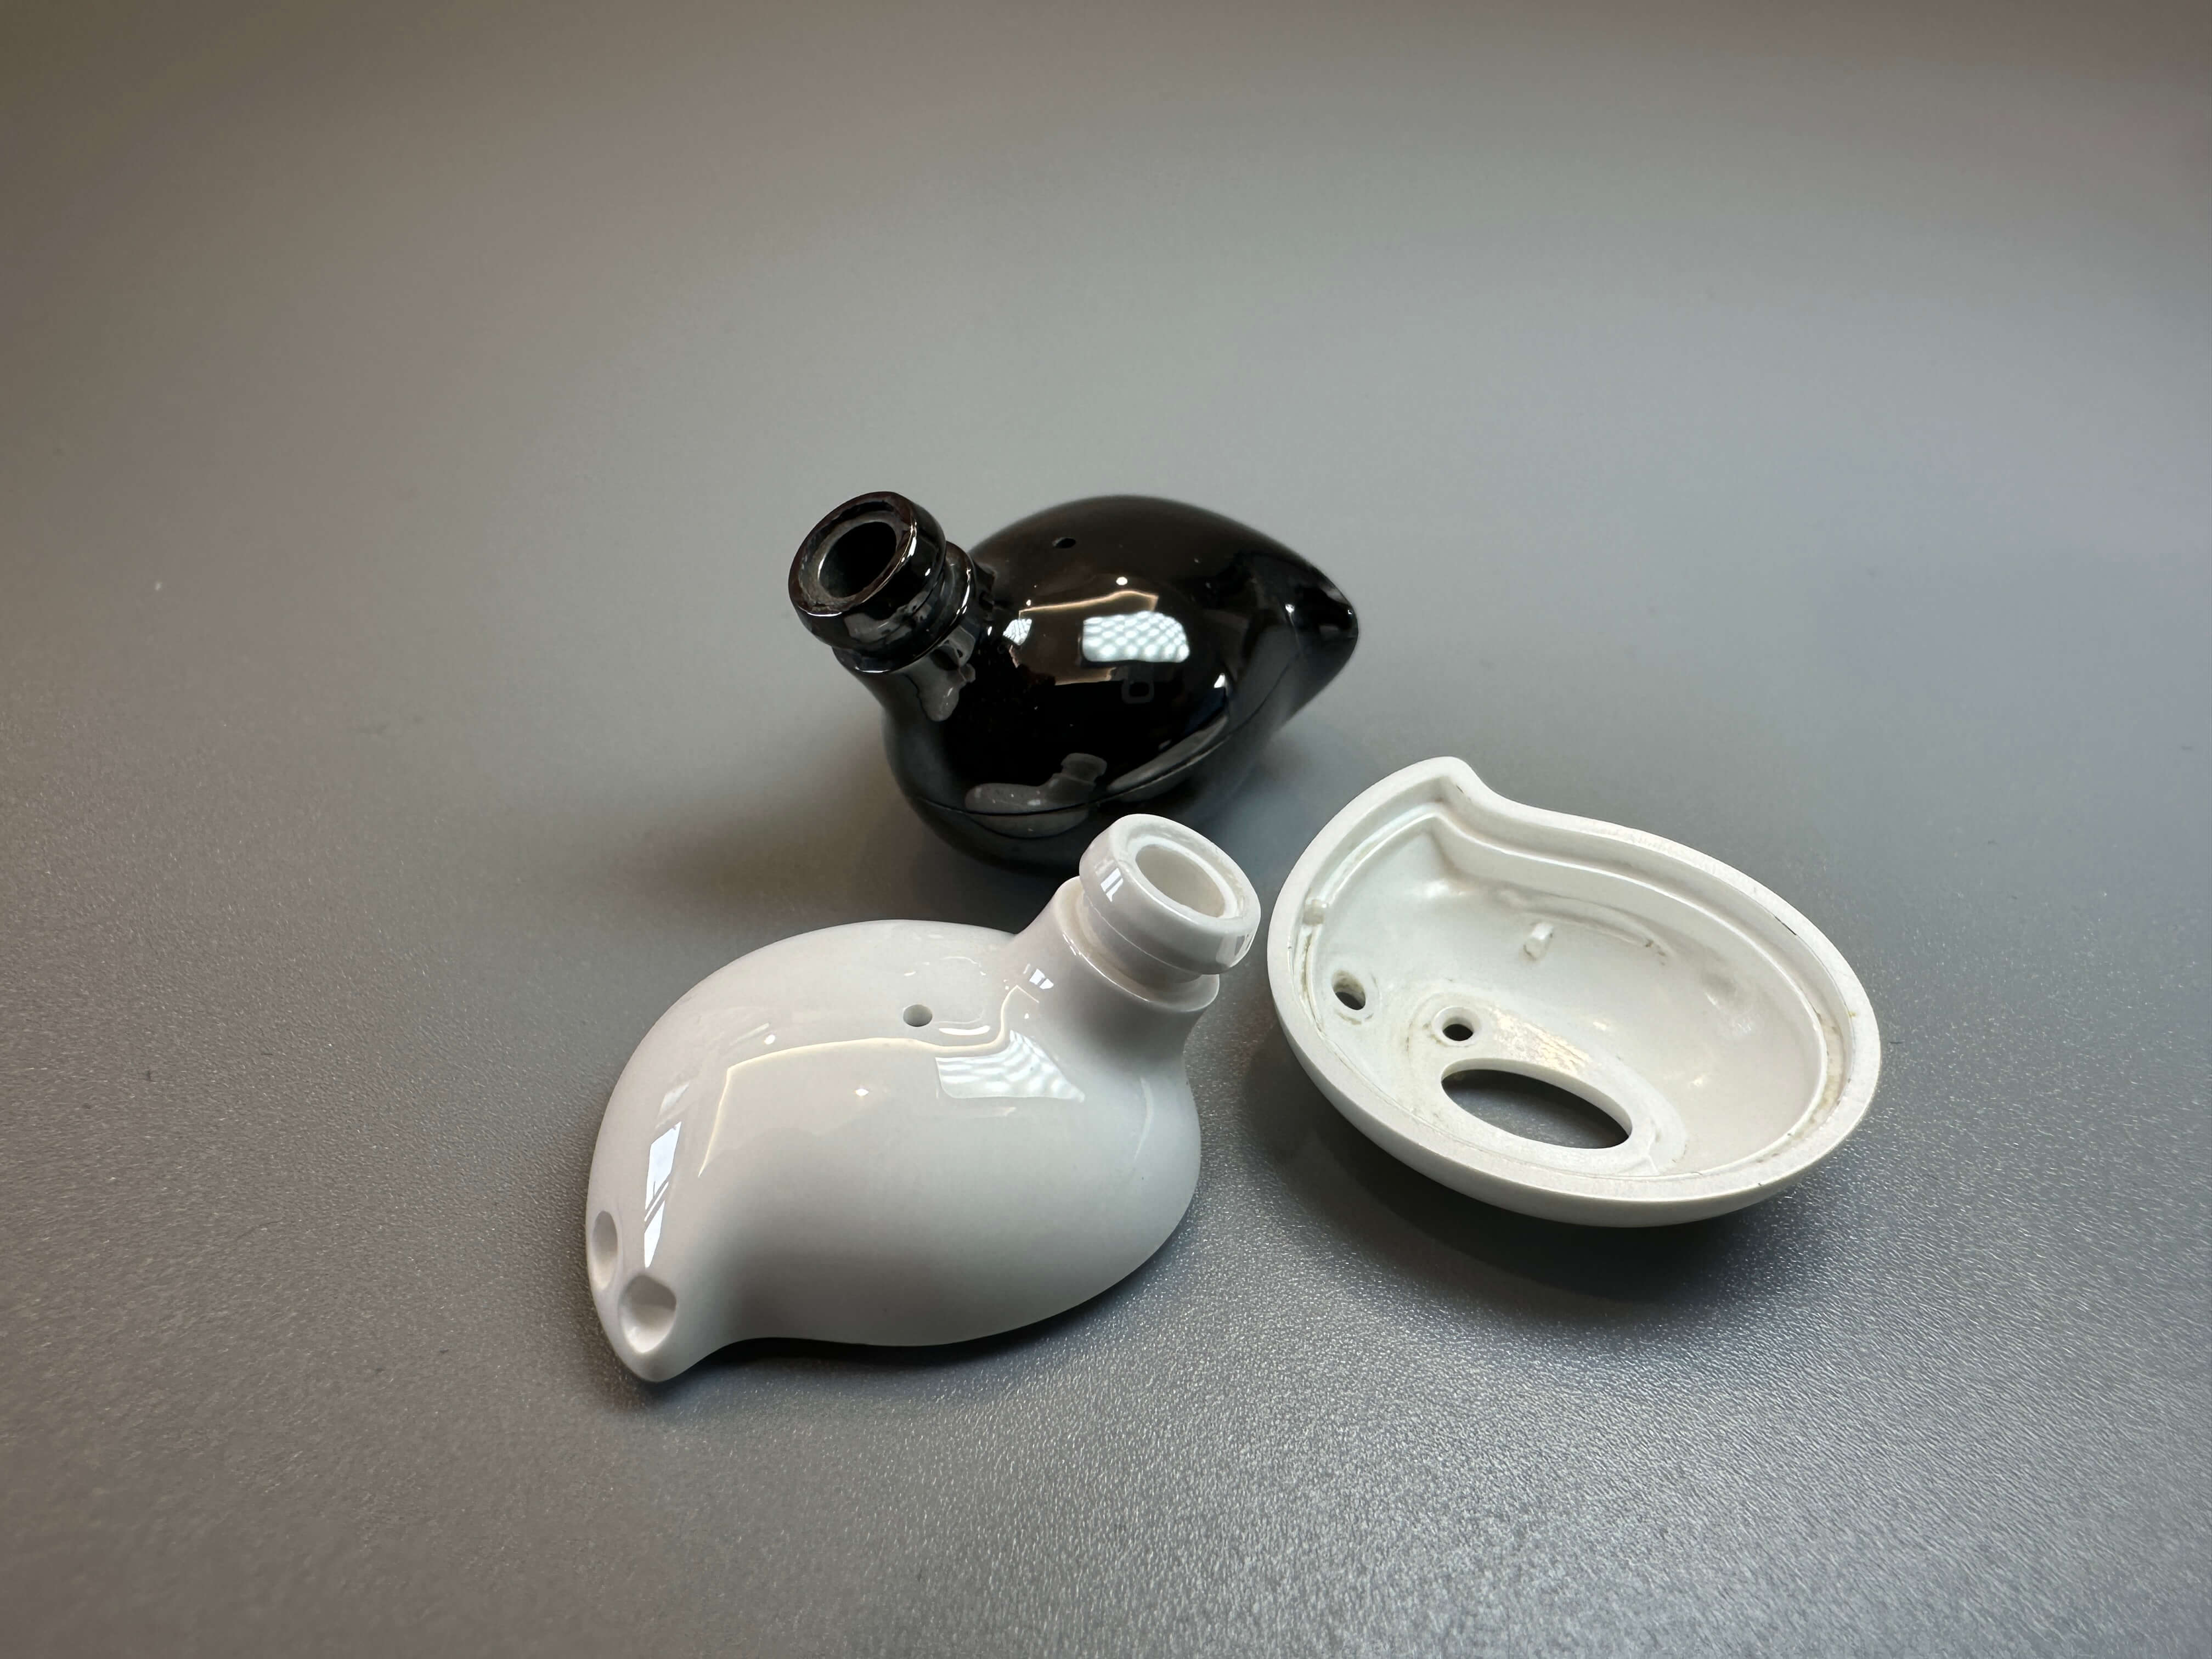
Difficulty: thin-wall parts face the highest risk at demolding and sintering - insufficient support means the green body deforms or breaks easily, while a high-gloss mold also readily traps air or leaves flow marks during injection. Requiring A-grade gloss on top of that stacks two demanding constraints on process control.
Solution: upfront Moldflow simulation predicts fill path and density distribution in the thin-wall zone, paired with a dedicated demolding fixture to reduce green-body stress; feedstock melt index and chain length tuned to wall thickness and design intent to improve success rate; staged debinding balances shrinkage across the cavity; post-sinter ball-mill polishing to Ra 0.02-0.03μm.
Customer value: your design doesn't need to trade off thin walls against cosmetic finish - with sound geometry, both can be achieved together.